Contents
You make nine decisions when you choose one, and each one affects the next. The material sets the exposure limit. The exposure limit sets the type of enclosure. The enclosure sets what the process equipment inside it can look like. The process equipment sets how the whole system is cleaned and validated. If you make these decisions in the wrong order, the project costs more.
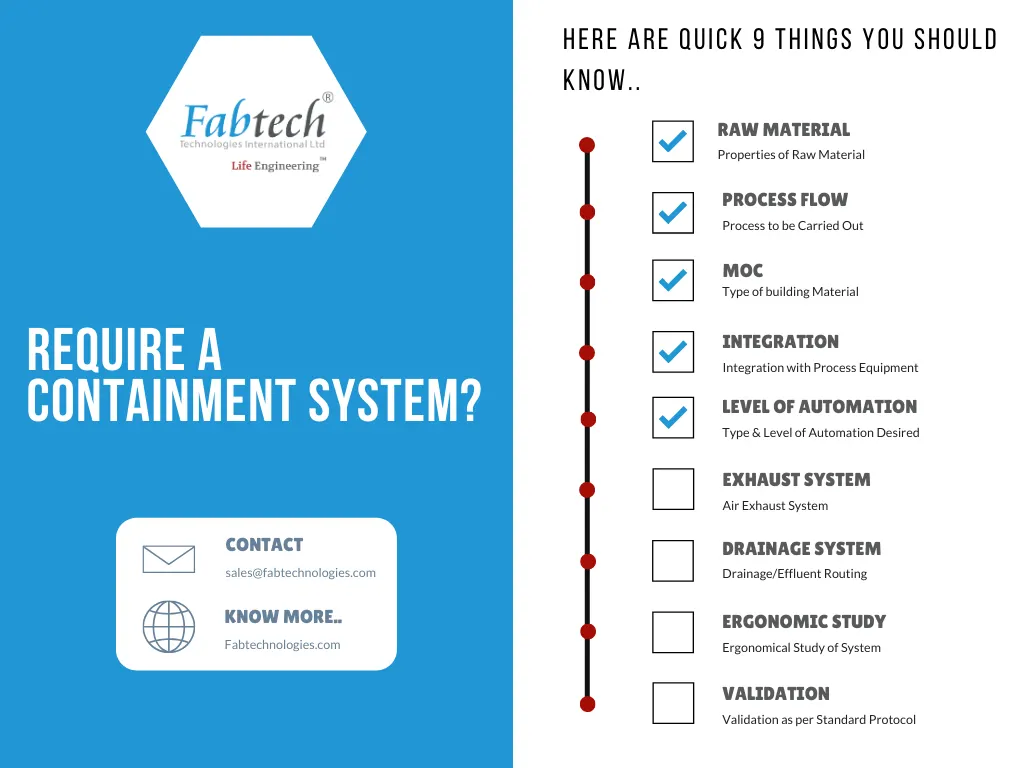
The nine points below explain how to choose the right containment system.
Which enclosure each OEB band needs
The nine points below use Occupational Exposure Limits (OEL). An OEL is the highest amount of a compound that is allowed in the air an operator breathes. Most buyers start with an OEB (occupational exposure band) instead. A band groups compounds by how potent they are. This section shows which enclosure each band needs.
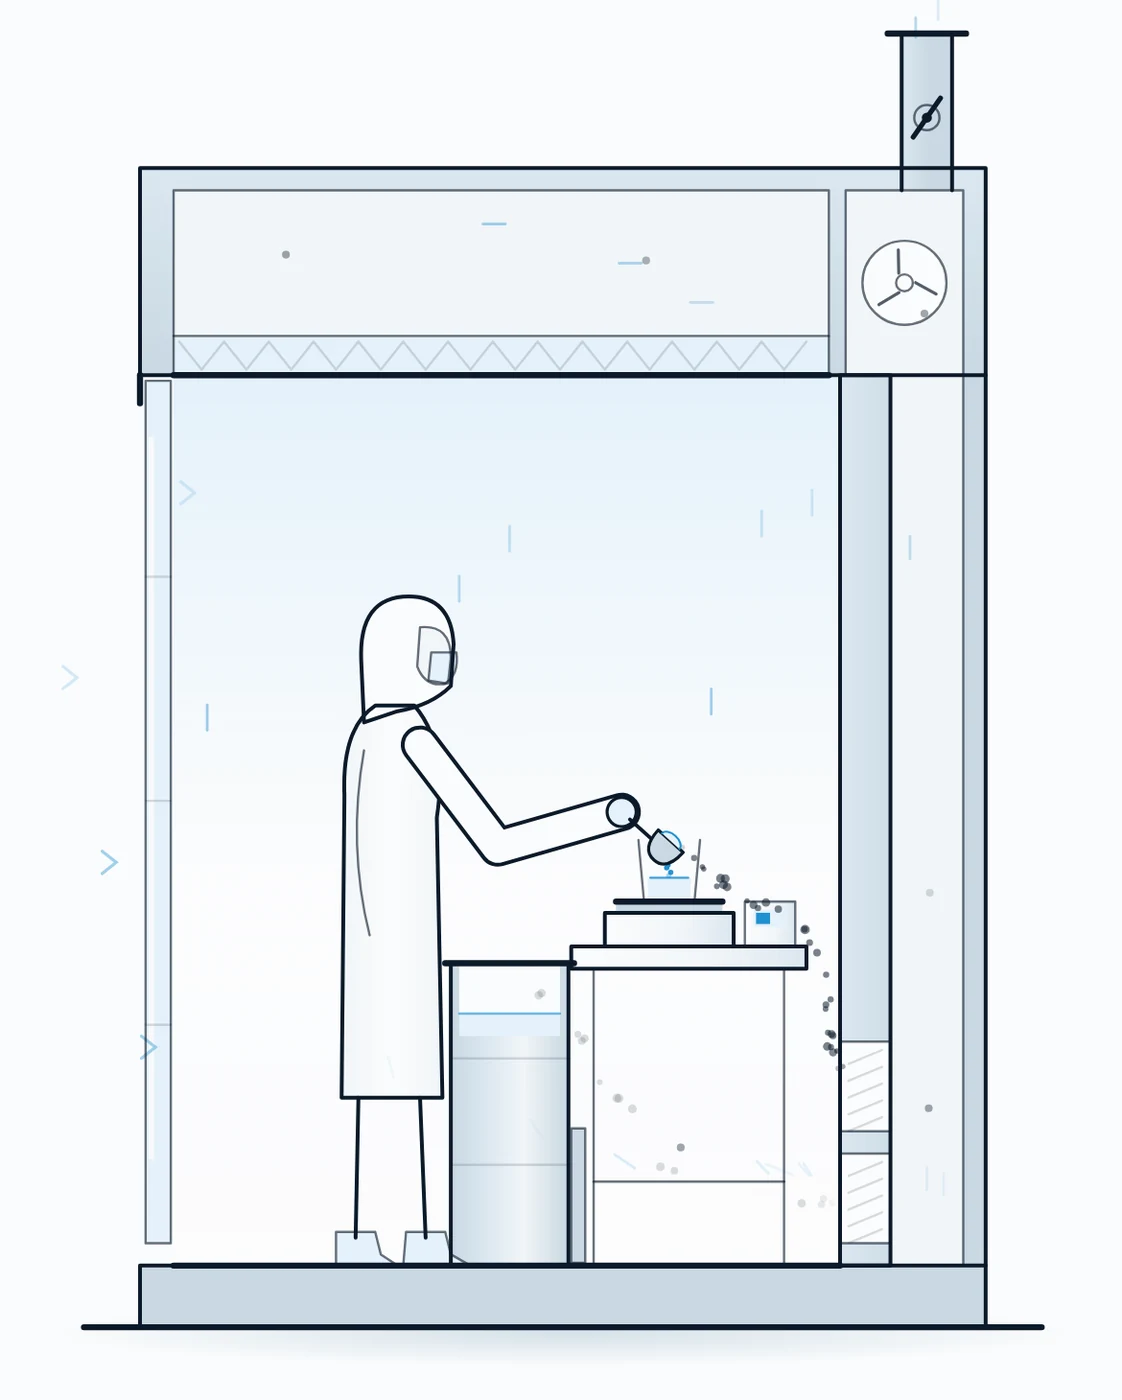
- Lower bands can use an enclosure with an open front. It protects the operator by controlling the direction of the airflow. One example is a sampling and dispensing booth, rated up to OEB 2 with add-ons. It is faster to work in, and much cheaper.
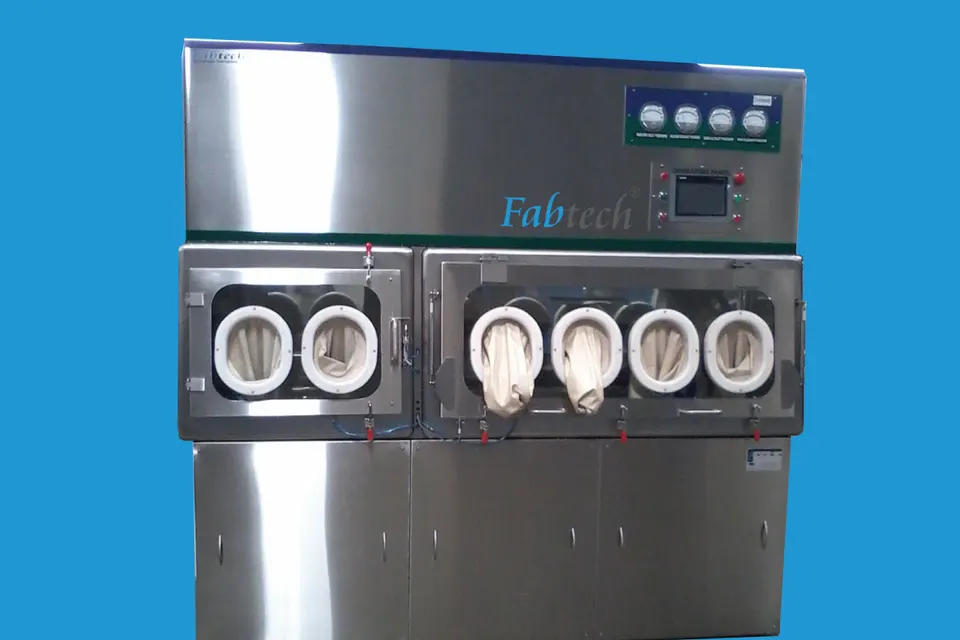
- OEB 4 and OEB 5 need a sealed boundary, not one made by airflow direction. This means a containment isolator at negative pressure, with glove access and contained transfer. Negative pressure means the air pressure inside is lower than in the room, so air flows in and not out.
- Above that, containment is no longer only a safety measure. It becomes the process itself. The enclosure specification then decides the design of the plant, instead of following it.
This dividing line is fixed. It is not a matter of preference. An open-front booth cannot give the protection of a sealed boundary, whatever is added to it.
1) Raw materials
Start with the materials you will process. Their properties decide which system you need. Check the Occupational Exposure Level (OEL) of each material with care. Check its physical and chemical properties too.
Some materials need special care during handling and processing. For example, the APIs (active pharmaceutical ingredients) used in new products are becoming more potent. So the system should be able to keep the production area safe. It should also keep a specific environment while these compounds are handled, such as a set relative humidity and temperature.
2) Process flow and review
Write down the process flow in detail. Then do a containment review for each step, including the quantity of material handled. Review each of these:
- Material in
- Material out
- Manipulation
- Decontamination
Material moves from one process step to the next in a contained way. The transfer method must suit the OEL level. Decontamination means removing the compound from surfaces. The decontamination method and procedure must be clearly defined for both the process equipment and the containment system.
3) Material of construction (MOC)
For rigid systems, the MOC (the material the system is built from) is SS 316 L, a stainless steel grade. The material of the gaskets and manipulative devices must be FDA compliant. It must also be compatible with the molecules being processed. Standard electrical execution is NFLP (non-flameproof). FLP (flameproof) execution is recommended for solvents. It also depends on the characteristics of the molecules being handled.
For flexible systems, the MOC is PU based (PU is polyurethane, a flexible plastic). Risk assessments decide which manipulative devices and gaskets are used. The whole system is made for single use.
4) Integration
The process equipment that is joined to the containment system must also suit it. A detailed engineering study makes sure the joint between them is airtight. A second study checks that each manipulation is practical. It also checks the decontamination and cleaning process. The mechanical, electrical and control systems of the process equipment and the containment system must work together as one.
In practice, this is why containment is specified around a named machine. It is not specified in general terms. A capsule filling isolator, a tablet compression isolator and a reactor charging isolator each have a different integration problem.
5) Level of automation
The main aim of containment solutions is the safety of products and operators. They control exposure to high-potency substances or reduce contamination. One way to improve efficiency is to reduce or remove human intervention.
The control systems for the containment and the process equipment must work together. Then the operator uses one set of instructions for both. There are many possible combinations, but they come down to two types:
- HMI PLC based control system: a simple touch-based system that mostly controls a single piece of equipment. HMI (human machine interface) is the touch screen. PLC (programmable logic controller) is the controller behind it.
- SCADA based control system: a system with many functions that controls multiple equipment and processes at the same time. SCADA stands for supervisory control and data acquisition.
6) Exhaust system
The exhaust air system is one of the most important parts of an isolator, at any level. It matters most when the required containment level is 1 µg of the potent compound per cubic metre of air.
Inside a barrier or isolator built for containment, the airflow should give a clear view of the work. It should also remove any heat from the process equipment inside.
Whether the air is recirculated or exhausted depends on any special atmosphere the process needs. If the process needs low humidity or an inert atmosphere, the system should recirculate the air to reduce cost. The exhaust air must be filtered to capture the potent materials before it is released.
7) Drainage system
The drainage system is another critical part of an isolator. The waste must be disposed of in the correct way.
The isolator usually has a floor that slopes to the drain, and the drain area is easy to see. The chamber is cleaned with manual spray guns and a hose, or with fixed stainless steel piping and spray balls. A floor drain with a valve lets liquid waste leave safely. To avoid liquid waste, cleaning cloths soaked with alcohol can be used instead. Waste water drains through a bottom seat valve into the waste water collection tank. It is then discarded.
8) Ergonomics study
An ergonomics study checks that operators can work in the system with ease and safety. It uses a replica of the containment system. Many detailed tests make sure everything matches the real operations. After this, the final 3D drawing is prepared and manufacturing begins.
Ask for this step. In a sealed enclosure, the operator reaches everything through gloves. If a reach is awkward in the mock-up, operators will change how they do the task in production. Containment failures start this way.
9) Validation
Validation is proof that the system works as designed. Process equipment is validated to the standard protocol. For containment systems, there is also a combined validation of the process equipment and the containment system. It includes:
- Leak testing of the entire system (this is a critical test)
- Air cleanliness level, including HEPA integrity testing, velocity profile and particle count
- Sound levels
- Light intensity
- Drainability
- Process equipment interlocking with the containment system
After the system is commissioned, OEL validation is conducted using surrogate materials. A surrogate material is a safer substance used in place of the potent compound. This test checks the whole system design. It is done once, by certified hygiene professionals working closely with the end user. The results are independently certified for OEL exposure.
Ask every supplier for this test. Until a system is surrogate-tested and independently certified, its containment claim is only a design intent. It becomes a measured performance only after that test.
Fabtech's containment systems
Fabtech's containment systems can be used for tablet and capsule manufacturing, injectables, APIs and customised solutions. The pharmaceutical isolators page shows the full range.
One decision comes before all nine points above: whether the enclosure protects the product or the person. The page on the difference between positive and negative pressure containment explains this choice. For a custom process that needs its own enclosure below room pressure, see the negative pressure system.
Our Life Engineers can help you with any further information.
FAQ
What is a pharmaceutical containment system?
It is an enclosure and its air handling. Together they keep a potent compound away from the operator and the environment. It can be an open-front booth that works by controlling airflow direction. It can also be a sealed, negative-pressure isolator with glove access.
What are the different types of containment?
There are two broad types. Rigid systems are made of SS 316 L. Flexible single-use systems are made of PU. Rigid systems are permanent and can be cleaned. Flexible systems are disposed of after use, so there is no cleaning validation to do.
How do I choose a containment system?
Follow the nine points on this page in order. Start with the OEL of your material. The exposure limit decides the enclosure. The enclosure decides what process equipment fits inside it. The process equipment decides how the system is cleaned and validated.
What containment level does a potent compound need?
Lower OEB bands can be handled in a booth. OEB 4 and OEB 5 need a sealed isolator at negative pressure. Requirements can be as low as 1 µg of compound per cubic metre of air. The tighter the figure, the more the exhaust system design decides the build.
What material of construction is used?
SS 316 L for rigid systems, with FDA-compliant gaskets and manipulative devices. PU for flexible single-use systems. Electrical execution is NFLP (non-flameproof) as standard. FLP (flameproof) is used where solvents are handled.
How is a containment system validated?
The process equipment and the containment system are validated together. The tests include leak testing, sound, light, drainability and interlocking. They also check HEPA integrity, velocity profile and particle count. Then certified hygiene professionals carry out OEL validation with surrogate materials. The results are independently certified.
Is containment performance actually measured, or just designed?
It is measured. After commissioning, OEL validation with surrogate materials turns a design intent into a certified figure. It is a one-time test, carried out with the end user.
Should the exhaust be recirculated or discharged?
It depends on the atmosphere the process needs. If the process needs low humidity or an inert atmosphere, recirculating the air costs less to run. In both cases, the exhaust air is filtered before it is released.
What industries use pharmaceutical containment systems?
They are used in tablet and capsule manufacturing, injectables, and API and HAPI (highly potent API) production. They are also used in customised applications in fine and specialty chemicals.