Contents
Coating is used on tablets, granules, crystals, powders and pellets. The sections below cover the four types used in the industry and the parameters that control them. They also cover the defects that appear when those parameters go wrong.
Why tablets, granules and pellets are coated
Senior citizens and children find it difficult to swallow or gulp some oral dosage forms. The cause may be the tablet size, and possibly the bitter taste of the drug. This happens in many households, where children dislike taking medicines because of the taste.
Coating is a process that covers the outside of a tablet with a layer of another substance. This layer gives benefits that the uncoated tablet does not have. Pharmaceutical coating can be applied to a wide range of solid oral dosage forms, including tablets, granules, crystals, powders and pellets. Coating has been used for almost a century. It is still an important part of modern medicine making, and today it uses advanced machines and technology. Coating systems for OSD (oral solid dosage) units serve many purposes.
Taste and odour. Different active pharmaceutical ingredients (APIs, the substances that treat the illness) and excipients (the other ingredients in the tablet) have different tastes or odours. Some may be mildly bitter and some very bitter. To cover this taste or odour, film-forming agents, taste-masking agents and flavouring agents are added with the coating ingredients.
Stability. Many drugs are sensitive to light, moisture and atmospheric oxidation, which is damage caused by oxygen in the air. Stabilizers added to the coating ingredients help protect the drug from light, moisture and atmospheric oxidation.
Elegance. The uncoated core is pharmaceutically inelegant, which means it does not look good. Pharma-grade pigments or shining materials added to the coating ingredients improve the look of the tablet.
Staining. A coloured API moves easily out of the tablet. It stains the patient's clothes and hands. Granules or core tablets with such an API are coated with soluble cellulose materials.
Release profile. The drug release profile is when and how fast the drug is released in the body. Coating can change or control it. This works with osmotic release oral delivery systems, enteric (delayed-release) coating, and sustained-release coating.
Incompatibility. Sometimes two substances in one product are incompatible, which means they may react with each other. Coating can reduce this risk. One of the two substances is coated to keep it apart, or a pellet that was first compressed into a core is coated.
Oral solid dosages make up a large part of medicine manufacturing. The reasons are that patients take them as prescribed (patient adherence), they are efficient to make, and each dose is very precise. Coating lets one core meet several of these needs at once.
The four types of coating in the pharmaceutical industry
Tablets need different coatings, based on what they contain and who will take them. There are four types of coating in pharmaceutical industry use: sugar coating, film coating, particulate or pellet coating, and compression coating.
| Type | What is applied | Typical weight added | Time |
|---|---|---|---|
| Sugar coating | Sucrose-based solution, in stages | 60 to 80% | 3 to 5 days |
| Film coating | Polymer film, 20 to 100 µm | 2 to 3% | single stage |
| Particle, granule or pellet coating | Sprayed solution or dispersion onto a core particle | product-specific | product-specific |
| Compression coating | A dry compressible layer pressed around a core | product-specific | single stage |
Sugar coating
Some medicines taste sweet at first. Then, for a few minutes after swallowing, they leave a bitter taste in the mouth or a feeling of a lump in the throat. Such a tablet is masked with one of the coating methods: sugar coating.
Sugar coating was developed by the sweet-making (confectionery) industry. The pharmaceutical industry largely borrowed it from there. It is still used today.
The sugar-coating process needs skilled manual work and could last for 3 to 5 days. However, it is less popular in the pharmaceutical industry than it once was. The work is laborious and the process time is long. It needs skilled and trained staff. After sugar coating, the tablet cannot be embossed, printed or labelled. The coating also makes the tablet larger and heavier.
In the coating pan, a sucrose-based (sugar) solution is applied to the tablets again and again. Sugar coating runs in five stages: seal coating, sub coating, smoothing, colour coating, and polishing and printing.
Film coating
Film coating applies a thin polymer-based layer to the OSD, which may be a tablet, granules or pellets. The layer is between 20 and 100 µm thick. It is a single-stage process, and it is faster. Film coating adds only 2 to 3% to the tablet weight, while the sugar coating process adds 60 to 80%. Film coating also allows embossing or printing on the tablet.
However, film coating is very capital intensive, which means it needs a large investment. It requires a massive facility for production.
A film coating is usually made of these parts:
| Component | Examples | Function |
|---|---|---|
| Polymer | Hydroxy Propyl Methyl Cellulose (HPMC) | Film-forming agent |
| Plasticizer | Poly Ethylene Glycol (PEG) | Provides elasticity |
| Pigment or opacifier | Sunset yellow, Quinoline yellow, Brilliant blue, Titanium dioxide, Ponceau 4R, Iron oxide yellow and red | Colouring agents |
| Vehicle | Purified water, isopropyl alcohol, methylene chloride | Solvent to dissolve the rest |
The vehicle is the liquid that carries the coating, and the choice matters. An aqueous (water-based) film coating needs more drying energy and a longer process. A solvent-based coating dries faster. But it also needs solvent recovery, limits on residual solvent, and fire protection.
Particle, granule and pellet coating
Particle, granule or pellet coating places a thin layer around a core particle, granule or pellet. The coating is applied by physical deposition. This means a solution or dispersion is sprayed onto the cores and then dried, and this forms the film.
This method improves overall flowability, which means the particles flow more easily. It protects unstable or reactive substances against air, humidity, light and oxidation. It improves mechanical properties. The particles resist wear (abrasion) better and are easier to compress. It improves texture, appearance, odour and taste. It also gives controlled and sustained release, and so improves drug dissolution.
The particle coating techniques in use are microencapsulation and the fluid-bed spray configurations. Microencapsulation puts very small particles inside a thin shell. The fluid-bed spray configurations are top spray, bottom spray (Wurster), and tangential or rotary spray. Which of these particle coating methods suits a batch depends on three things. They are the core, the film thickness needed and how much mechanical stress the particle can take. Our guide to evaluation methods of pharmaceutical pelletization explains how coated pellets are then checked.
Compression coating
Compression coating is similar to tablet making. The core or coated tablets are surrounded by compressible excipients. This layer prevents drug incompatibilities. It protects the drug from light, humidity, oxidation and other environmental factors. The process uses no solvent and no drying. For this reason, it is still used for products that cannot tolerate a solvent or drying.
Enteric and modified-release coating
An enteric coating is a film that does not dissolve in stomach acid. It does dissolve further down, in the small intestine, where the pH is higher (less acidic). It is used for two reasons. The first is to protect a drug that acid would destroy. The second is to protect the stomach from a drug that would irritate it. The pharmacopoeias, the official books of medicine standards, call the result delayed release.
Sustained release and controlled release work differently. They do not delay the start. They control the rate. There are two ways to do this. In the first, the drug diffuses out slowly through a polymer film. The second is an osmotic release oral delivery system. Here, water is drawn in through a semipermeable coat, which lets water pass in. The water then pushes the drug out through a laser-drilled orifice, a very small hole. In both cases, the coat is the mechanism that controls release.
This is important in manufacturing. A functional coating, meaning a coating that controls how the drug is released, is a critical quality attribute in its own right. A critical quality attribute is a property that must stay within its limits for the product to pass. If a cosmetic film coat runs 5% light, only the appearance is affected. If an enteric coat runs 5% light, the tablet fails dissolution.
Pan coating and fluid bed coating
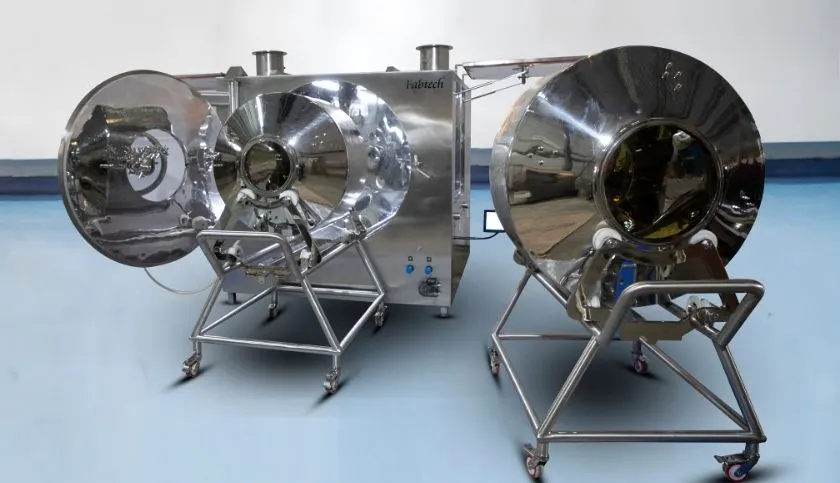
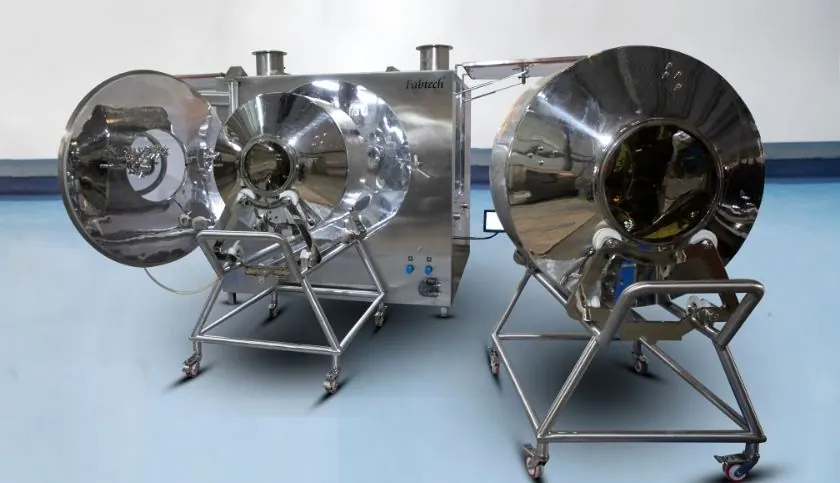
Pan coating turns tablets in a rotating perforated drum, which is a drum with holes. The coating solution is sprayed onto the moving bed of tablets, and warm air is drawn through it. Fluid bed coating holds the cores up in an air stream and sprays them while they are in the air. The right method depends on the core.
Tablets are coated in a pan. They are large enough and strong enough to tumble without breaking. A perforated drum also gives the airflow needed to dry an aqueous film at production rates. That machine is the auto coater.
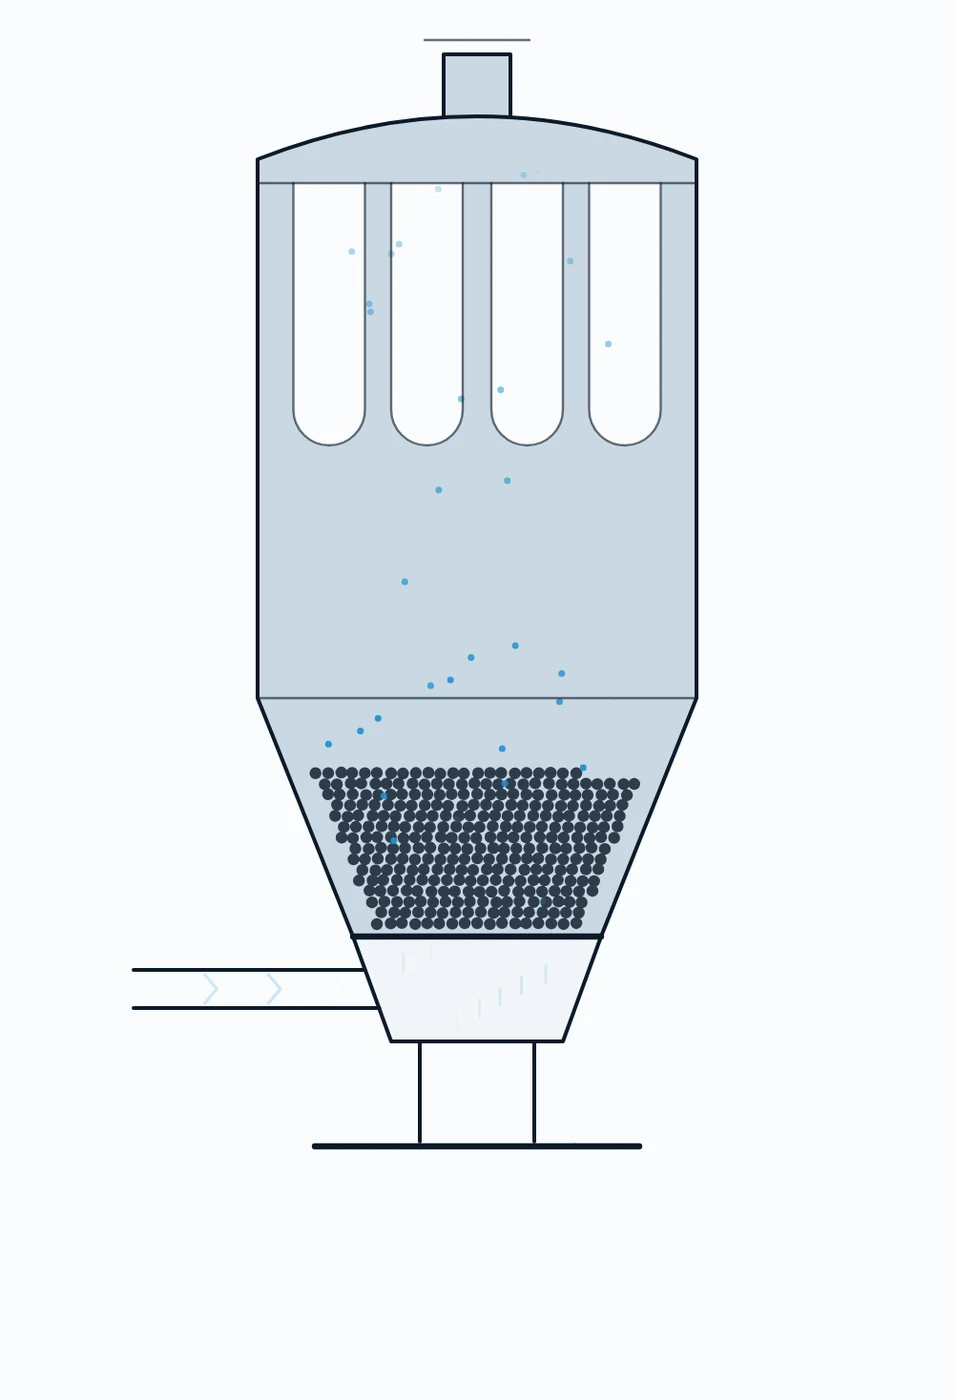
Granules, pellets and particles are coated in a fluid bed. There is no other practical way to reach the whole surface of a small core. The bed keeps every particle separated and moving. So the film thickness is even from one particle to the next, and also across the whole batch.
Top spray suits taste masking and protective coats. Bottom spray, called the Wurster configuration, gives the most uniform film. It is the usual choice for modified release. The equipment is the fluid bed processor, run as a coater.
Coating process parameters
A set of parameters controls coating. Each one is monitored, validated and set for each product, so that quality is repeatable at maximum yield. Three things decide whether production-size batches can be coated successfully. They are the instruments selected to measure the right parameters, the way the coating process is optimized, and the way it is scaled up.
| Parameter group | Parameters | What it controls |
|---|---|---|
| Air | Inlet airflow, outlet airflow, air velocity, pressure drop across the inlet-outlet airstream | How much drying capacity reaches the bed, and whether the bed moves as intended |
| Temperature | Inlet air temperature, outlet air temperature, bed temperature, spray temperature | How fast the tablet surface dries. This decides whether a droplet spreads on the tablet or dries before it lands |
| Humidity | Inlet air humidity, outlet air humidity | How much drying the air can really do. This changes with the season unless the air is conditioned |
| Spray | Spray flow rate, spray concentration, atomizing air pressure | Droplet size, and how much solution arrives per unit of time |
| Mechanical | Speed of the drum | How often each tablet passes through the spray zone |
All these parameters control one balance. The coating solution must reach the surface slightly faster than the air can dry it, or the film never forms. It must also arrive slightly slower than the surface can take it, or the bed becomes wet. Every defect below comes from losing this balance in one direction or the other.
Coating defects and what causes them
Most coating defects can be diagnosed from the process parameters. This is why the parameters are worth logging, even on a batch that passes.
| Defect | What it looks like | Usual cause |
|---|---|---|
| Twinning | Two tablets stuck face to face | The bed is too wet, or the drum speed is too low for the tablet shape. Flat-faced tablets are the worst |
| Picking and sticking | Coating lifted off, or tablets stuck to the pan | Too much wetting. The spray rate is too high for the drying capacity |
| Orange peel | Rough, dimpled surface | Droplets dry before they spread. The spray is too far away, the atomizing pressure is too high, or the inlet air is too hot |
| Cracking or splitting | Film split over an edge or an emboss (a raised or pressed-in logo) | The film is too brittle, usually because there is too little plasticizer. Or the core expands |
| Colour variation | Patchy or uneven colour across a batch | Poor pigment dispersion, uneven spray distribution, or a coating time that is too short |
| Erosion | Edges worn, logo worn down | Processing time too long, drum speed too high, or a core too friable (too weak) to coat |
| Peeling | Film separates from the tablet in sheets or flakes | Poor adhesion between film and core. The cause is a core surface issue, too little tack (stickiness), or a coat that dried too fast or too slow to bond |
| Blistering | Bubbles under the film | Air, moisture or solvent trapped under the coat, often from drying too fast. Or gas escaping a porous core through a part-cured film, which is a film that has not fully set |
| Bridging | Film pulled out of an emboss so the logo fills in | The film shrinks as it dries. The solids content is too high |
The pattern is consistent. Twinning, picking and sticking are defects at the wet end. They mean the solution is arriving faster than the air can remove it. Orange peel and colour variation are defects at the dry end. They mean the opposite. Erosion and cracking are mechanical defects. They point to a problem with the core or the drum rather than with the spray.
The coater cannot repair a core that is already fragile when it arrives. That is why the properties of a good tablet granulation are checked long before coating starts.
Automation, control and the coating equipment
The coating process in the pharmaceutical industry has been practised for a very long time. In that time, pharmaceutical coating technology has moved from manual pans to fully instrumented systems.
Current Good Manufacturing Practice (cGMP) is the set of quality rules that medicine makers must follow. cGMP and regulatory authorities worldwide require the greatest care in the equipment used to prepare tablets and to run the coating operation. The same care applies to the design of manufacturing facilities, the materials used to build them, and their layout.
Coating processes are managed through a rising range of automation and control levels. When the process parameters are controlled automatically, the equipment gives essential functions. The first is batch parameter data logging, which records the settings of each batch. The second is a list of alarms, warnings and safety interlocks. Each one has a specific and immediate action attached, such as a cycle stop or an operator alert.
The recipe is the set of process settings for a product. It can be automated, with different user levels such as operator, supervisor and manager.
21 CFR Part 11 is the US FDA (United States) rule for electronic records. Automated coating systems are built to 21 CFR Part 11 for the records they create. So the batch data logged during a run is a controlled record rather than a simple printout. Fabtech's equipment includes the auto coater and the fluid bed processor. They are designed to meet the critical process parameters above and to reach the end-product quality parameters.
Our experts advise on the different pharmaceutical coating processes. They deliver the solution for a specific coating application. This pharmaceutical processing and coating service covers the specification, build, installation and qualification of the pharma coating step. Qualification is the set of tests that proves the equipment works as specified. The service is more than the supply of a machine on its own.
People researching the pharmaceutical coating equipment market usually want one of two things. Some want a report on who supplies what. Others want a machine for a specific product. This page answers the second need.
Fabtech manufactures pharmaceutical coatings equipment as part of a wider process range. So a coating system is specified for the production line it will work in. It is not bought as a machine alone. This covers tablet coating and pharma pelletizing coating systems, the utilities and controls behind them, and the qualification that follows.
If you are looking for a supplier for one machine, the auto coater page above has the specification. If the coating step is part of a plant, the turnkey projects page describes the industrial and processing scope around it. In both cases, the same engineering company builds it. So one company is accountable for the coating service from start to end.
Coating is one step in an oral solid dosage line. The OSD manufacturing process page shows the full sequence. The step before coating is on granulation techniques. Our wider machine range is on process equipment for pharma.
FAQ
What is coating in pharma?
Pharmaceutical coating puts a thin outer layer on a solid oral dosage form, such as a tablet. The coating can hide a taste, resist stomach acid or control the release rate. It can also protect against light and moisture, or give a surface that can be printed. It is applied to tablets, granules, crystals, powders and pellets.
What are the types of coating in the pharmaceutical industry?
Four: sugar, film, particulate or pellet, and compression coating. Sugar coating applies sucrose in five stages over three to five days. Film coating applies a polymer layer of 20 to 100 µm in one stage. Particle coating sprays small cores in a fluid bed. Compression coating presses a dry layer around a core.
What is the difference between sugar coating and film coating?
Sugar coating adds 60 to 80% to the tablet weight. It takes three to five days across five stages, and the tablet cannot be printed or embossed afterwards. Film coating adds 2 to 3% and runs as a single stage. It allows embossing and printing. Film coating needs more capital equipment.
What is an enteric coating?
It is a film that does not dissolve in stomach acid. It dissolves in the small intestine, where the pH is higher. It protects a drug that acid would destroy, or it protects the stomach from a drug that would irritate it. The pharmacopoeias call the result delayed release.
What equipment is used for pharmaceutical coating?
Tablets are coated in a perforated pan, in an auto coater. Granules, pellets and particles are coated in a fluid bed, by top spray or by bottom spray in the Wurster configuration. Both are controlled by airflow, temperature, humidity, spray rate and drum or bed movement.
What are the coating process parameters?
The air parameters come first: inlet and outlet airflow, temperature and humidity, air velocity, and the pressure drop across the airstream. Then come the bed and spray temperatures, spray concentration and flow rate, atomizing air pressure, and drum speed. Each one is monitored, validated and set for each product.
What causes twinning, picking and orange peel in tablet coating?
Twinning, picking and sticking mean the bed is too wet. The solution is arriving faster than the air can dry it. Orange peel is the opposite. The droplets dry before they spread. The cause is an inlet that is too hot, an atomizing pressure that is too high, or a spray distance that is too great.
What is Wurster coating?
It is bottom-spray fluid bed coating. The spray nozzle sits at the base of the bed. The cores move up past it in a controlled circulation. This gives the most uniform film thickness across all the particles. It is the usual choice for modified-release pellet coating.