Granulation techniques
Most pharmaceutical powders cannot be compressed into a tablet as they are. Granulation is the step that makes them ready for the tablet press. Granules flow well. They do not separate on the way to the die, the cavity in the press where the tablet is formed. They compact into a tablet of the right weight every time. The granulation techniques of tablets come down to three routes. The route is chosen to suit the drug molecule. The equipment a plant already has does not decide it.
- A binder solution is a liquid that makes particles stick together.
- Direct compression means pressing the powder straight into tablets.
On this page
What granulation is, and why powders are granulated
Granulation is the process of forming granules from a powdery or solid substance. They are usually irregular in shape, but they can also be made round and uniform. Granulation techniques change and improve the properties of active pharmaceutical ingredients. These are the active substances in a medicine, also called APIs.
In pharmacy and across the pharmaceutical industry, the granulation process is the stage between weighing out a formula and powder tableting. On their own, the actives have low bulk density, poor flowability and poor binding. Bulk density is the weight of powder in a given volume. In this state the actives cannot be compressed into tablets.
Granules make powders flow better and give uniform mixtures. They stop the powder from separating, which is called segregation. They give dust-free formulations. They ensure that each unit carries the same amount of drug. This is called content uniformity. They also help the powder mix compact better. These are the reasons for granulation.
Wet granulation adds one more reason. It is the main one among the advantages of wet granulation. It can bond powders that will not bond by mechanical force alone. That is why wet granulation is still the default route for actives with poor flow and low density.
It is also why granulation is important in the pharmaceutical industry. The quality of a granular tablet or a granule medicine is set at this stage. If the granulation is wrong, no later step can correct it.
Granules flow more freely than powders from the hopper, or feeding container, into the die cavities of tablet presses. Granules also have a smaller surface area than the same volume of powder. This makes them more stable, physically and chemically, than the powder. They are less likely to cake or harden. In some cases a solvent wets them far more easily.
Granulation, compression and coating are three steps in one chain. A fault made at the first step can rarely be corrected at the third. So the quality of a manufactured tablet or capsule is set by the granulation process itself. This happens well before the granules reach a tablet press or a capsule filler. Good granulation gives fewer tablet defects, improved yield, higher productivity and reduced downtime.
In one case, granulation can be skipped. It is the ideal choice where the formulation allows it. But most substances need to be granulated first.
Granulation technology has changed a lot since the days of a mixer and a tray dryer. A modern granulation system on a production line joins mixing, wetting, drying and sizing into one controlled sequence. Advanced granulation technology runs the same sequence as a continuous operation. The reason for the stage has not changed. The stage makes granules, and the tablet is made from the granules.
- Granules are small groups (agglomerates) of finer powder particles.
- Roller compaction presses the powder between rollers.
- An excipient is any ingredient in a medicine other than the active.
- Granulators are described by their shear, which means how much mechanical force they apply.
- Mouldable binders are solid at room temperature but melt in the temperature range of 50 to 80°C.
The three types of granulation
Granules are prepared by two classical methods, dry granulation or wet granulation. Melt granulation is the third route. It uses heat in place of a liquid binder. So the granulation methods of tablets fall into three groups. In short, there are 3 types of granulation. Each type of granulation suits a different kind of molecule.
| Method | How the bond is made | Typical reason to choose it |
|---|---|---|
| Dry granulation | Mechanical compaction, by roller compaction or slugging | The molecule is sensitive to moisture or heat |
| Wet granulation | A granulation liquid, with or without a binder | Poor flow, low bulk density, high dose, no natural binding |
| Melt granulation | A binder that melts with heat and becomes solid when it cools | Neither water nor solvent is acceptable |
Dry granulation includes dry mixing, roller compaction, and slug-and-deslug. Slug-and-deslug compresses the powder into large, rough tablets called slugs. It then mills and re-sieves the slugs to size. Roller compaction and slug-and-deslug both build the granule with pressure. Neither of them uses liquid. That is what lets a moisture-sensitive product run on the same production line. Wet granulation includes aqueous (water-based) and non-aqueous (solvent-based) granulation.
Wet granulation
Wet granulation is a widely used technique. It mixes the active pharmaceutical ingredient with a granulation liquid, with or without a binder, to form a wet mass. This is called wet massing, and the wet mass is then made into granules.
As a flow chart, the steps of wet granulation run in seven stages:
- Weigh and sift the actives and excipients.
- Dry mix them.
- Add the granulating agent (the binder solution) to form a wet mass.
- Wet milling breaks the wet mass down to a workable size.
- Drying takes it to the target moisture.
- Dry milling and sifting bring it to the final size distribution.
- The granules then go on to blending.
These granulation stages are the same whichever machine is used. What changes is how many of them happen in one vessel.
More detail
Wet granulation has seen many more technical and technological innovations than dry granulation. It is used for molecules that do not suit the dry route. These molecules have a high dose, poor flow, low bulk density, and no binding properties of their own.
Wet granulation is carried out in two ways. The first way moistens the powder or powder mixture. It then passes the mix through a screen, and the mesh size of the screen gives granules of the size needed. Dry heat then dries the granules.
The second way uses a fluid bed processor. Inside it, the particles are strongly dispersed and held suspended. A liquid excipient is sprayed onto them, and they are dried in the same vessel.
The choice of aqueous or non-aqueous solvent depends on how sensitive the molecule is. Aqueous processes are considered safer and more cost-effective. Non-aqueous processes are for molecules that water would break down. They use organic solvents such as isopropyl alcohol, dichloromethane and chloroform as the binder solution. Safety is critical during this process. All equipment must be flameproof and placed in a dedicated area. All safety measures must be followed.
Steam granulation is a variation of wet granulation. It uses steam as the binder instead of water. Steam spreads more evenly through the powder and moves into it faster. It also gives a better heat balance during drying. Steam granules are more spherical and have a larger surface area, so the drug dissolves faster from them. Processing time is also shorter.
Steam granulation uses no organic solvent. So it avoids the residual-solvent limits and the fire risk of non-aqueous processing. Freshly distilled steam is sterile, so the total count of microbes can be kept under control.
Granule strength and density depend on the amounts of solution and binder, and on the mechanical action applied. So the equipment affects the granule as much as the recipe does.
Shear can be low, medium or high. A low-shear granulator uses very little force to combine the powders and the binding solution. A high-shear machine works the wet mass much harder. Medium-shear machines are between the two. The aim is the correct granule density, and no single granulator suits every powder.
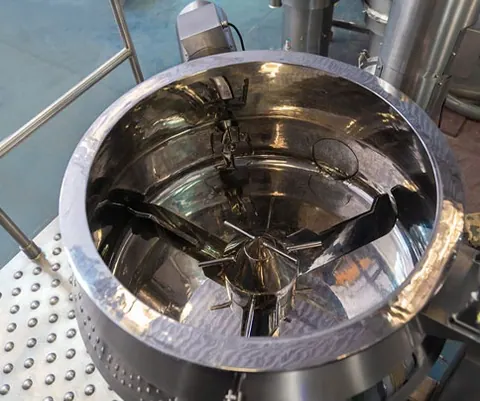
Whichever machine is chosen, its handover follows the equipment qualification sequence. It is not handed over on a delivery note alone. Fabtech supplies both high-shear mixers and fluid bed processors. The high-shear versus fluid-bed comparison explains where each one fits. The machine for the high-shear route is the high shear mixer granulator, also called a rapid mixer granulator (RMG). Some actives are so potent that the transfers between machines must be contained. For these, the same stages are piped together as a closed loop granulation line instead of running as separate units.
Dry granulation
The dry granulation process uses roller compaction or slugging. Dry powder is passed through a roll compactor and then granulated to a uniform particle size. Granules made this way are porous and highly compressible. This allows fast disintegration, and the release time can be modified.
More detail
Dry granulation is almost always chosen because of the molecule. This process is excellent for drugs that are moisture-sensitive. It is also excellent for molecules that are sensitive to other factors, such as temperature. Where the formulation allows, manufacturers can also choose molecules with specified particle sizes and directly compressible grades of excipients. This reduces how much granulation is needed at all.
Melt granulation
Melt granulation is also called hot melt granulation. It uses a binder that melts at a workable temperature, instead of a granulation liquid.
More detail
The powder and binder are heated and mixed until the binder softens and joins the particles together. The mix is then cooled so these joins become solid. Nothing has to be dried afterwards. So there is no drying step and no solvent handling.
Melt granulation suits molecules that cannot be exposed to water and cannot tolerate an organic solvent either. It is not suitable where the API itself is thermolabile, which means damaged by heat. This is because the whole method depends on applying heat.
Foam granulation is the other route that reduces liquid. The binder is added as an aqueous foam instead of a sprayed liquid. So less binder and less water are needed to wet the powder. The foam can be added faster than a sprayed liquid, with no harm to the granulation or the tablet. There are no spray nozzles, so there are no over-wetting or plugging problems.
Foam spreads the binder evenly and shortens drying. This makes it useful for water-sensitive formulations. Immediate release and controlled release formulations need much less binder with this process.
Wet or dry: how the method is chosen
The molecule decides the method. Ask these questions in this order:
Is it moisture sensitive?
If yes, use the dry route or melt granulation. Water is the first thing to rule out.
Is it heat sensitive?
If yes, use dry granulation. Melt granulation cannot be used.
Does it flow and bind on its own?
If yes, direct compression may remove the need to granulate at all.
Is the dose high, the bulk density low, or the flow poor?
That is the typical case for wet granulation.
What release profile is required?
The release profile is how fast the drug is released. Dry granulation makes porous, highly compressible granules. They disintegrate quickly and allow the release time to be modified.
Here is the difference between wet and dry granulation. Wet granulation builds the bond with a liquid and then removes the liquid. Dry granulation builds the bond with force and never adds liquid at all. Those are the methods of granulation in practice. The dry and wet granulation choice is made on the molecule.
What a good granule looks like
Granulation characterization is the set of measurements that describe a batch of granules before it reaches the tablet press. They include particle size, flow, density and moisture. Whichever route is used, the granules must meet five attributes before they reach the press. A granulation process is set up to meet these five.
Critical process parameters are the process settings that change these attributes. They depend on the method. Binder quantity and addition rate apply to any wet route. Impeller and chopper speed and wet massing time apply to a high-shear mixer. Inlet air temperature and drying end point apply to a fluid bed.
| Attribute | What it controls | The target |
|---|---|---|
| Densification | Whether the dose plus excipients fits the tooling size | Poured density of the dried granules between 0.55 and 0.65 g/cm³ |
| Flow property | Whether the press fills evenly at speed | Near-spherical granules. Measured by angle of repose, including on a rheometer |
| Granule size distribution | Tablet appearance, hardness and cohesiveness | A natural distribution curve from 24 mesh to 100 mesh |
| Compressibility | Whether mixed powders compact into a tablet at all | (Tapped density − poured density) ÷ poured density × 100; ideally 10 to 30%. The same tapped-to-poured comparison expressed as a ratio is the Hausner Ratio |
| Moisture content | Stability, and how the mass behaves under compression | Typically 1 to 3%, by loss on drying |
Densification means making the granules denser. It is wanted only until the dose and its excipients fit the tooling used for compression.
Porosity also matters here. Porous materials compact better. Good porosity comes from controlling the density of the wet granules and choosing the right mill sizes. If the density is too high, compression gets harder. Well-densified granules, compressed at a medium force, give tablets with high density and good cohesive strength. These tablets still disintegrate quickly in water.
Flow property depends on particle shape. It does not depend on particle size distribution. Free-flowing granules are near-spherical, because irregular shapes cause friction and poor flow. High-shear mixers and fluid bed granulators are designed to produce this near-spherical shape.
Size distribution decides how the tablet looks and how well it holds together. A mix of mostly separate granules with very little fine powder gives rough tablets. These tablets have low hardness and low cohesiveness. The best case is a careful mix of large and small granules, fines included.
Fine powders can also behave well. Direct compression excipients such as microcrystalline cellulose and lactose grades are mainly fine particles. Even so, they flow and compress without trouble.
The full specification for a granule that is ready to compress is on the properties of a good tablet granulation page.
Granules as a dosage form
Not every granule becomes a tablet. Some granules are used for oral solutions or suspensions. These granules carry colourants, flavourings and other ingredients with the active. So the finished solution or suspension has all the features of a liquid formulation. Tablet compression machines also turn granules into effervescent tablets, dispersible tablets, mouth-dissolving tablets, melt-in-mouth tablets and modified-release tablets.
Sometimes the active is only a small part of the tablet. Then correct granulation is what makes it possible for each unit to contain the right amount. The active may not match the other ingredients in particle size, density, flow, moisture or compressibility. If so, it will segregate during blending or on transfer to the press.
One answer is to granulate the active on its own and then blend it. The better answer is usually to mix it well with the other ingredients first, and then granulate the blend. The bond inside each granule then stops the ingredients separating before compression.
Everything in a tablet other than the active is an excipient. Excipients help powders flow more easily, which matters when they are transferred into the die cavity. They also improve how the formulation behaves in the press and how the active performs.
There are four main classes of excipient. Binders fuse the powders and link the particles. Fillers add bulk to the tablet. Lubricants stop powder sticking to the press. Disintegrants help the tablet break up after it is swallowed.
Compressed tablets must meet pre-determined specifications for uniformity of dosage units, hardness, friability, disintegration time and dissolution rate. Friability is how easily a tablet crumbles. The tablets must also stay stable until the batch expiry date. This is only possible with the right granulation technique and a validated process.
FAQ
What is granulation in pharma?
Granulation is the process of forming granules from a powder. The granules flow well, resist segregation and compress into tablets of consistent weight. Granulation is a preparation step. It is carried out before compression or capsule filling.
What are the three types of granulation?
Wet granulation, dry granulation and melt granulation. Wet granulation uses a granulation liquid, with or without a binder. Dry granulation uses mechanical compaction, by roller compaction or slugging. Melt granulation uses a binder that is softened by heat and set by cooling.
What is the difference between wet granulation and dry granulation?
Wet granulation builds the bond with a liquid, then removes the liquid by drying. Dry granulation builds the bond with mechanical force and never adds liquid. That is why dry granulation is the route for moisture-sensitive molecules.
Why are powders granulated at all?
Most active ingredients have low bulk density, poor flow and poor binding on their own. In that state they cannot be compressed into a tablet. Granulation corrects the flow, prevents segregation and removes dust. It also makes the content uniform from tablet to tablet.
What is wet granulation used for?
It is used for molecules with a high dose, poor flow, low bulk density and no binding properties of their own. One way moistens the powder, passes it through a screen, then dries it. The other way uses a fluid bed processor. It sprays the liquid onto suspended particles and dries them in the same vessel.
What equipment is used for granulation?
Roller compactors and slugging presses are used for the dry route. High-shear mixers and fluid bed processors are used for the wet route. Granulators are described by how much mechanical force they apply: low, medium or high shear. No single granulator suits every powder, because the aim is a specific granule density.
What is a granule in pharmaceuticals?
A granule is an agglomerate of smaller powder particles. An agglomerate is a small group of particles held together. It is usually irregular in shape but can be made near-spherical. Granules are compressed into tablets or filled into capsules. They are also supplied as a dosage form in their own right, for oral solutions and suspensions.
What density should granules be before compression?
The poured density of the dried granules before compression should be between 0.55 and 0.65 g/cm³. The size distribution should run from 24 mesh to 100 mesh.