Contents
What OSD means in pharma
OSD is the abbreviation for oral solid dosage. An OSD product is a medicine taken by mouth in solid form. It can be a tablet, a capsule, a soft gel, an effervescent, a gummy or a pill. Other fields use the letters OSD for other things. In pharma, and in the pharmaceutical industry in general, OSD means oral solid dosage and nothing else.
The term is used across the whole company. So you will see it in many combinations: OSD plant, OSD formulation, production OSD, OSD department. OSD means the same thing in each one. Only the thing being described changes.
| Term | Meaning |
|---|---|
| OSD | Oral solid dosage. This is the full form, in pharma and in every OSD company |
| OSD tablet, OSD drug, OSD medicine | A drug product in oral solid form, not a liquid, a cream or an injection. OSD drugs are dispensed as tablets and capsules more often than in any other form |
| OSD formulation | What the product is made of: which API, which excipients, in what proportions, and what release profile it must have. OSD formulations are developed before manufacturing begins |
| OSD manufacturing | Making the product at scale, from dispensing to a packed and released product |
| OSD plant | The facility and its lines: the rooms, the equipment, the utilities and the flows |
| Production OSD, OSD department | The people and shifts who run the OSD lines. Production OSD means the manufacturing department, not a product |
| QA and QC in OSD | QA means quality assurance. QA runs the system that gives the same quality every time. QC means quality control. QC tests the material |
Oral solid dosage is one of several dosage form groups. The others are liquids and syrups, semi-solids such as creams and ointments, and sterile products, including injectables. Some plants make both liquid and solid dosage forms. They make them in separate suites with separate flows. This is because the contamination risks and the room conditions are different. This page covers only the solid route.
An OSD product is the API plus its excipients. The API (active pharmaceutical ingredient) is the molecule that has the medical effect. Excipients are all the other ingredients: binders, fillers, lubricants, disintegrants and coating materials. Together, they decide whether the API can be made into a tablet at all.
Formulation and development
The process begins with formulation and then development. In this stage, the active pharmaceutical ingredient (API) is combined with suitable excipients to create a stable and effective dosage form.
Formulation development aims for the right drug release profile, better bioavailability and regulatory compliance. Bioavailability is how much of the drug reaches the blood, and how fast. For a highly potent API, special technology is used to reach good solubility and keep the medicine effective. A formulation is only well defined when the excipients and the API are both well understood.
Formulation is the oldest part of the work. Aspirin came from willow bark. Almost every early medicine came from a plant, a root, a bacterium or a fungus. Chemistry was first used to take the active ingredient out of these sources and make it more potent. Formulation today decides what must surround the active ingredient. The aim is that it reaches the patient intact, is released at the right rate and has a usable shelf life.
Decisions made in formulation limit every step that follows. A moisture-sensitive molecule, one that water damages, rules out the wet route before any machine is chosen. A high dose sets the tablet size. The tablet size sets the tooling, and the tooling sets the press. A modified-release profile makes the coating step critical instead of optional.
Scale-up of oral solid dosage forms is the stage where a formulation that worked at laboratory scale is proved at production scale. It is a separate discipline, and it has its own ways to fail.
Fabtech's work begins where oral solid dosage formulation services and oral solid dosage development services end. Fabtech's oral solid dosage services are engineering services. They cover process design, the equipment, the utilities that support it, the rooms and qualification. They cover small and large scale. At the small end are single units for laboratory and pilot production. At the large end are complete production lines for powder processing and oral solid dosage forms.
The OSD manufacturing process, step by step
The OSD manufacturing process runs in this order: dispensing, sifting and milling, granulation, drying, blending, compression, coating and packaging. Quality control takes samples at set points throughout. Not every product uses every step. A formulation that can be compressed directly skips granulation and drying. An uncoated tablet skips coating. The remaining steps stay in the same order.
Dispensing
Dispensing means weighing out each raw material against the batch record, in a controlled area. This step sets what goes into the batch and how much. So it is done under a sampling and dispensing booth or a similar contained enclosure. The booth keeps airborne powder away from the operator. It also keeps cross-contamination out of the material. An error made here passes to every later step.
Sifting and milling
The dispensed powders pass through a sieve. The sieve breaks up lumps and removes material that is too large. If the range of particle sizes must be narrower, the powder is also milled. In practice, sieving, screening and milling are one stage, often on one set of connected machines.
Particle size affects the dissolution rate, the content uniformity and how the blend flows. Dissolution rate is how fast the tablet dissolves. Content uniformity means each tablet holds the same amount of drug. So a screening or milling step that is out of specification shows up as a compression problem four steps later. Particle sizers are the machines for this stage.
Granulation
Granulation is a size-enlargement process. The powdered API and excipients are stuck together (agglomerated) into larger granules. This improves how the powder mixture flows, how well it compresses and how uniform it is. The core granulation methods for pharma manufacturing are wet granulation, dry granulation and direct compression. The method is chosen based on the operating conditions, the formulation's properties and its requirements.
Dry granulation. This economical method suits compounds that are sensitive to temperature and moisture, where both must be tightly controlled. One dry technique is slugging. Slugging compresses small, dry particles into larger granules. The aim is a tablet with the right ratio of ingredients and the right amount of excipient. Roller compaction is the other dry route.
Wet granulation. This method is regarded as superior because it works without special excipients and gives good content uniformity. The method is adaptable and reproducible. It needs perfect dispersion and careful preparation of the granules. Its quick processing time makes soluble, low-dose medicines easier to handle.
Direct compression. Direct compression is a simpler and shorter process of mixing the ingredients. It works well with APIs that are sensitive to heat and moisture. With direct compression, tablets disintegrate into particles of API. After wet granulation, they disintegrate into granules instead. Because the tablet breaks down into API particles, its dissolution behaviour is different. This difference must be tested, not assumed. This method also helps avoid extreme compaction pressure during tablet production.
The granulation techniques page compares the three routes in full. It covers the equipment for each route and how to choose between them.
Drying
Wet granules are dried to a set moisture content before compression. The target range is narrow. If the granules are too wet, they stick in the press. If they are too dry, they lose the plasticity that lets them bond. Plasticity is the ability to change shape under pressure.
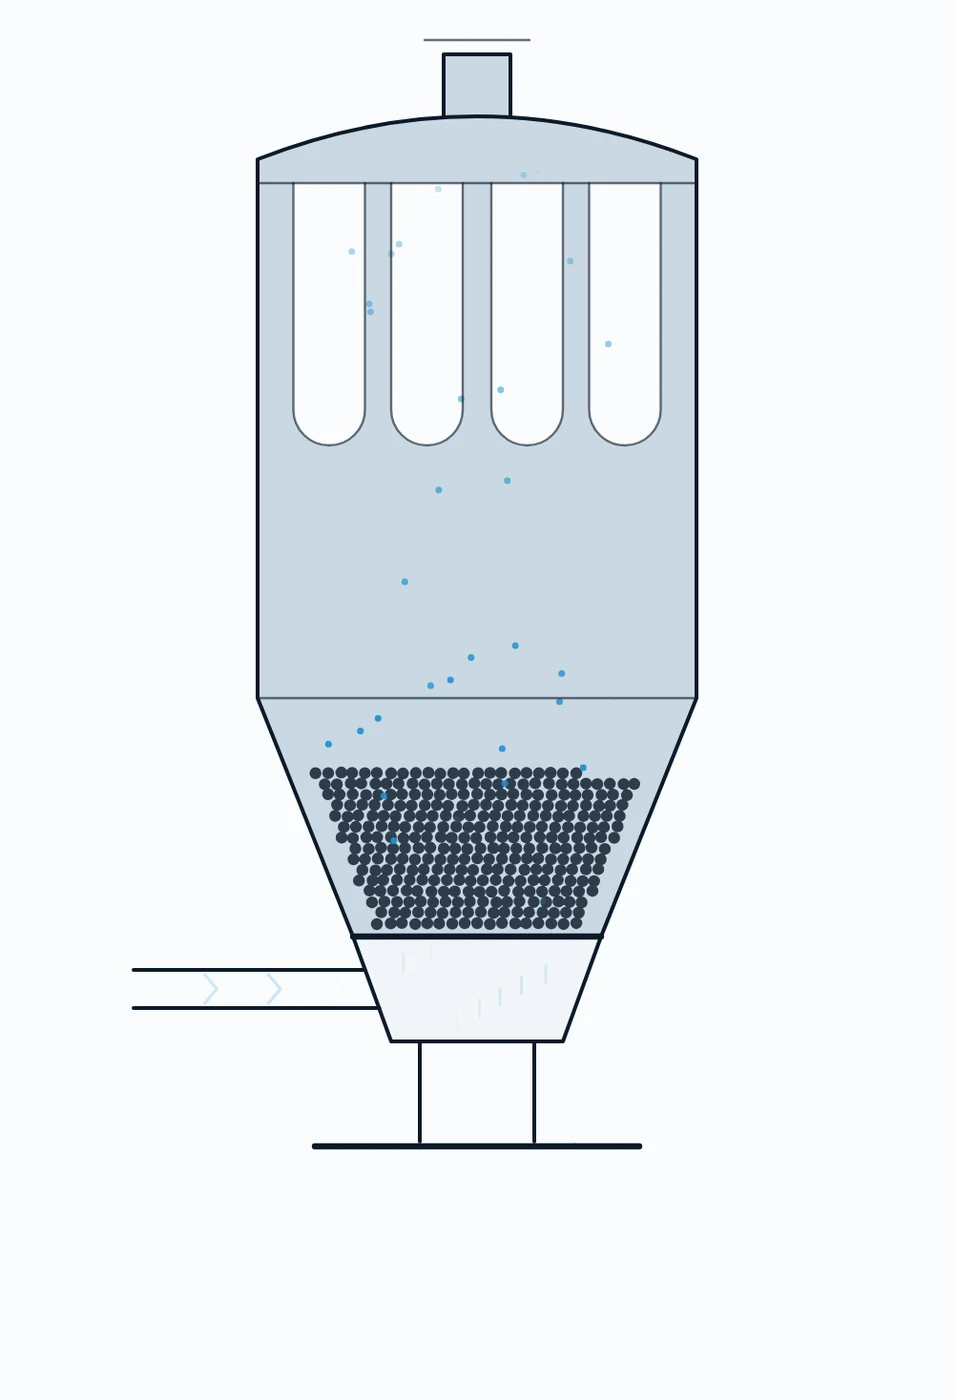
Drying is done in a fluid bed processor, which holds the granules up in a stream of hot air. For smaller batches, a tray dryer can be used instead. In a fluid bed suite, granulation and drying happen in the same vessel. This removes one transfer, and the contamination risk that comes with it.
Blending
After granulation, the granules may be blended with more excipients, such as diluents, disintegrants and lubricants. Blending spreads the API and excipients evenly through the whole mixture. This improves content uniformity, so each tablet is the same as the next. The main aim of blending is to mix the ingredients well enough. This is done with mixing equipment and blenders such as octagonal blenders, V blenders, bin blenders and conta blenders. The pharmaceutical blenders page shows the four that Fabtech builds, and which shell suits which job.
Too little blending is a problem, and so is too much. Over-blending a mix that contains lubricant coats the granule surfaces and makes the tablet weaker. So blend time is a validated parameter. It is fixed by trial and then kept the same.
Compression
Compression is known to be one of the most difficult steps. It can directly affect the hardness of the tablet. The hardness in turn affects whether the tablet holds together (dosage form integrity) and its bioavailability. In this step, a tablet press presses the granules or the blend into tablets. A tablet press is a high-speed mechanical machine.
The press squeezes the ingredients precisely into the required tablet shape: round, oval or scored. A scored tablet has a line across it so it can be broken. The compressed tablets must meet the physical and chemical properties specified for the tablet. They must also have the right hardness, thickness and weight.
What the press can achieve depends on the earlier steps. Before the granule reaches the die, the mould inside the press, it must meet five attributes: density, flow, size distribution, compressibility and moisture. The properties of a good tablet granulation page gives the specification for each. For capsules, the same blend goes to a capsule filling machine instead of a press.
Coating
In the tablet coating process, a thin layer of coating material is applied to the tablet surface. The coating gives the dosage form properties that an uncoated tablet does not have.
Equipment such as auto coaters for a granulation line makes the coating operation effective. Coating does several jobs at once. It protects the drug from the environment and makes the tablet easier to swallow and more stable. It can also mask the taste or change how the drug is released. The amount of coating on the tablet surface is critical to how well the oral dosage form works.
Film, sugar and enteric coating each meet a different need. A coating pan that is not set correctly causes defects such as twinning, picking and orange peel. The cause of each defect can be found in the process parameters. The pharmaceutical coating page covers both the coating types and the defects. The machine itself is covered on the page for the auto coater.
Packaging
Medicines must be packaged with the greatest care. After the tablets are manufactured and coated, they are packed carefully to keep out heat, air and water, which may change the drug's properties.
Primary packaging places the tablets in blister packs, bottles or other suitable containers. Secondary packaging, such as labelling and cartoning, gives information and protects the product during distribution. To choose the package, you first find out the product's physical and chemical characteristics.
Containment: high-potency OSD
Potent products need containment systems. Pharmaceutical isolators are containment systems with built-in air filtration. They meet the need for high protection of people and product from outside contaminants. Positive pressure isolators help keep the product sterile by protecting it from contaminants. Negative pressure isolators protect people and the environment. They keep hazardous or toxic materials inside the isolator. The choice of granulation isolator system is a process decision, based on batch size and capacity.
On an OSD line, the occupational exposure band of the molecule decides the containment. The dosage form does not decide it. The occupational exposure band groups a substance by how much of it workers can safely be exposed to. With a high-potency API, the enclosure goes first onto the open handling steps: dispensing, granulator charging, discharge and compression. These are the steps where powder is exposed. Fabtech supplies the granulation isolator and the tablet compression isolator for these points. The wider aseptic containment range covers sampling, dispensing and reactor charging.
A HEPA filter stops particles. It does not stop gases or vapours. So solvents are controlled by ventilation and extraction. Filters do not control them. Containment reduces exposure. It does not remove the need for the handling controls around it.
Inside an OSD plant
An OSD plant is a facility laid out so that people, materials and waste move in one direction and never cross. The order of the process steps sets the order of the rooms. The order of the rooms sets the shape of the building. A description of the process leaves out oral solid dosage facility design. A real OSD plant cannot leave it out, because it is part of OSD manufacturing.
Flow. Materials enter through a dispensing and staging area. They move forward through granulation, drying, blending, compression and coating. They leave through packaging to a finished-goods store. People enter through changing rooms. Each changing room is sized for the classification of the area it leads to. Waste and returns leave by a separate route. Where two flows must meet, they meet through an airlock, a small room between two areas.
Classification and pressure. Classification sets how clean the air in a room must be. Non-sterile OSD areas are typically built to a classified but non-aseptic standard. ISO 14644 defines the airborne particle classes. For the areas nearest open handling, a GMP grade is sometimes specified as well. This is typically C or D, not the full EU-GMP A to D range, which is meant for sterile manufacture.
Either way, the level is set room by room, by the product and the step in that room. So one plant has several levels.
The pressure cascade is the pattern of air pressure from room to room. It normally runs positive, from clean rooms to less clean rooms. Rooms with potent or dusty operations are the exception. They are held at negative pressure to keep the powder in. Both patterns exist in the same building. The layout must be designed so that both work together.
Dust. Solid dosage manufacturing creates airborne powder every time material is moved in the open. To keep cross-contamination out of the next product, the plant uses dust extraction at the source, dedusting between compression and coating, and room air change rates that match the dust load. The air handling and clean air systems that do this are designed together with the rooms. They are not added afterwards.
Utilities. Granulation liquid, cleaning water and final rinses come from a purified water system. The system is sized for the plant's peak simultaneous draw. This is the most water the plant uses at one time. The system is not sized for the average use. Compressed air that touches the product is filtered and monitored. HVAC (heating, ventilation and air conditioning) holds the classification and the pressure cascade. It also holds the temperature and humidity that granulation and coating need to give the same result every time.
Cleaning. Every product changeover is a cleaning validation event. The plant must prove the equipment is clean before the next product starts. So equipment is chosen because it is easy to clean. It has as few dead legs as possible (pipe sections where liquid can stay behind). Its product-contact surfaces are easy to reach. It is cleaned in place where its shape allows. This is what makes a multi-product OSD plant workable. Without it, the plant would face a series of week-long changeovers.
Fabtech engineers OSD facilities as complete projects. A project covers the process design, the equipment, the utilities that support it and the rooms that hold it. OSD manufacturing design and construction, and the qualification at the end, are under one contract. This is what OSD facility turnkey engineering means in practice. The pharmaceutical turnkey projects page describes the scope. The equipment is on process equipment for pharma.
Batch and continuous OSD manufacturing
Batch manufacturing takes a set quantity through each step, one step at a time. Continuous manufacturing feeds material through a connected line at a steady rate. It defines a batch by time or by mass. It does not define a batch by vessel. Most OSD production in operation today is batch. Continuous OSD lines exist, and regulators have said clearly that they are acceptable. But continuous lines change what a batch is. So they also change what release testing means.
The main engineering difference is where the material waits. A batch plant has hold points between steps. At each hold point, the team can sample the material, test it and decide. A continuous line has no hold points. The control strategy moves onto the line itself, as process analytical measurement. This means instruments test the material while it moves. Material that goes out of specification is diverted in real time. It is not rejected at the end.
The choice is a business decision first, and a technical decision second. Continuous suits high-volume products with a long life, where the line runs for weeks. Campaign manufacture means making one product for a period, then changing to the next. Batch suits multi-product plants and campaign manufacture, which is what most of the industry runs.
Quality control, quality assurance and validation
Quality control is essential throughout the manufacturing process. It makes sure the product has the right quality and meets regulatory standards. In a pharmaceutical manufacturing plant project, quality control checks the raw materials, in-process samples and finished products. It checks them for identity, purity, potency, dissolution and physical attributes. It also checks features of the material such as appearance, usability, compatibility and dimension.
Quality assurance means running a complete quality management system that covers every part of OSD manufacturing. It includes writing standard operating procedures (SOPs), documentation control, deviation management, change control and compliance with regulatory guidelines. These processes make sure medicines meet all quality control standards, so they are fit for their intended use. In short, quality control tests the material. Quality assurance runs the system that gives the same result every time.
Process validation shows that the manufacturing processes consistently produce OSD forms of the desired quality. It needs tests of every process that affects product quality. The tests show that each process is reliable and gives the same result each time.
The tests include validation studies. Equipment qualification is part of these studies. It is a series of tests that show each piece of equipment performs reliably. Under the contract, a plant is handed over against this series. The tests run in this order:
| Stage (the DQ/IQ/OQ/PQ sequence, with an acceptance test before and after delivery) | What it establishes |
|---|---|
| URS, User Requirement Specification | What the equipment has to do, written before it is designed |
| DQ, Design Qualification | That the proposed design meets the URS |
| FAT, Factory Acceptance Test | That it works at the manufacturer's site, before it ships |
| SAT, Site Acceptance Test | That it still works at the user site, after delivery |
| IQ, Installation Qualification | That it is installed as designed, with its services connected |
| OQ, Operation Qualification | That it works across its specified range |
| PQ, Performance Qualification | That it gives the required result with real product |
Process qualification checks that the process meets the required standards and can be sustained. Cleaning validation gives a high degree of assurance that product contaminants are prevented and controlled.
A new OSD line is handed over against this sequence. The page on equipment qualification in pharmaceutical engineering explains it in full.
GMP and regulatory compliance
OSD manufacturing must comply with Good Manufacturing Practices (GMP) guidelines for pharmaceuticals. Compliance shows that the methods and processes follow accepted quality practices. The guidelines cover proper documentation, record-keeping, facility design, personnel training, and following safety and environmental regulations. Good manufacturing practice guidelines explains what this means in practice.
At the design stage, the important point is this: the building decides most of GMP. Documentation and training can be corrected later. Flows, classifications, room finishes and equipment access cannot be corrected without rebuilding. An OSD facility is designed to pass inspection under USFDA (United States), MHRA (United Kingdom), TGA (Australia) and WHO-GMP expectations. The design decisions that make this possible are made before the first wall is built.
Fabtech works with pharmaceutical companies to produce safe, effective, high-quality oral solid dosage forms. We bring process knowledge, the equipment, and knowledge of the regulations the plant must meet.
Our specialists work with you to understand what your pharmaceutical manufacturing plant project needs. This can be single units for lab and pilot production, or complete production lines for powder processing and oral solid dosage forms. The aim is to get you to market cost-effectively and in the shortest time possible. As with our complete OSD production line, we give complete solutions for turnkey pharmaceutical projects, from start to finish.
FAQ
What is OSD in pharma?
OSD stands for oral solid dosage. These are medicines taken by mouth in solid form: tablets, capsules, soft gels, effervescent tablets, gummies and pills. It is the form most medicines are dispensed in.
What does OSD stand for in pharma?
Oral solid dosage. Other fields use the same abbreviation for other things. Inside a pharmaceutical company, it means oral solid dosage.
What is the OSD process?
The steps are dispensing, sifting and milling, granulation, drying, blending, compression, coating and packaging. Quality control takes samples throughout. A formulation that can be compressed directly skips granulation and drying. An uncoated tablet skips coating. The remaining steps stay in the same order.
What is an OSD plant in the pharmaceutical industry?
A facility built to manufacture oral solid dosage products. Its layout follows the order of the process steps. Materials, people and waste move in one direction and never cross. Where flows meet, they meet through airlocks. Dust is extracted at every open transfer. Rooms with potent or dusty operations are held at negative pressure.
What is API and OSD?
The API is the active pharmaceutical ingredient, the molecule that has the medical effect. OSD is the form it is given in: a tablet or capsule taken by mouth. An OSD product is the API plus the excipients that make it into a dosage form.
What are the different types of OSD?
Tablets, capsules, soft gels, effervescent tablets, gummies and pills. Tablets are further divided into immediate release, modified release, enteric coated, dispersible and mouth-dissolving tablets.
What is OSD in medical use?
For a patient, it means the medicine is a solid taken by mouth. It is not a liquid, a cream or an injection. The form affects how quickly the drug is absorbed. It also affects where in the digestive tract the drug is released.
How is quality controlled in OSD manufacturing?
Quality control tests raw materials, in-process samples and finished product for identity, purity, potency, dissolution and physical attributes. Quality assurance runs the system around it: SOPs, documentation control, deviation management and change control. Process validation then shows that the process gives the same result every time.
What is OSD formulation?
It is what the product is made of: which active ingredient, which excipients, and in what proportions. These are chosen to reach a set release profile, bioavailability and shelf life. Formulation is decided before manufacturing, and it limits manufacturing. For example, a moisture-sensitive molecule rules out wet granulation before any equipment is chosen.
What is the difference between batch and continuous OSD manufacturing?
Batch manufacturing takes a set quantity through each step in turn. It has hold points where material is sampled and tested. Continuous manufacturing feeds material through a connected line at a steady rate. It defines a batch by time or mass, and it moves the control strategy onto the line itself.