For some time now, the HVAC sector has been adapting the equipment they manufacture to address environmental concerns. For a long time, this was a result of newer, more stringent environmental regulations, but in the past decade it has increasingly become proactive as sticking to the old ways is far more expensive than switching to newer green technologies.
The HVAC sector is continuously evolving as new technologies develop and new concepts come into play. Relying on green technologies has several economic benefits and not just the ability to decrease a plant's environmental footprint.
In this post, we talk about the advantages of Two-stage Treated Fresh Air Units and a small tweak to the system can result in huge cost and energy savings.
Treated Fresh Air Units (TFA) are also known as Fresh Air Handling Units (FAHU). Unlike Air Handling Units that are used to recirculate the air in an enclosed space, TFAs cater to large, fresh airflow and recovery needs by treating outdoor air using filters and condition it some degree using a cooling system. TFAs are used when the requirement is 100% fresh air with no recirculation of air or to feed the number of AHUs to fulfil their fresh air needs. To illustrate, in treatment of fresh air, if the ambient temperature was 36-40 degree Celsius, after treatment the temperature is brought down to 24-22 degree Celsius so that it doesn't increase the air conditioning load.
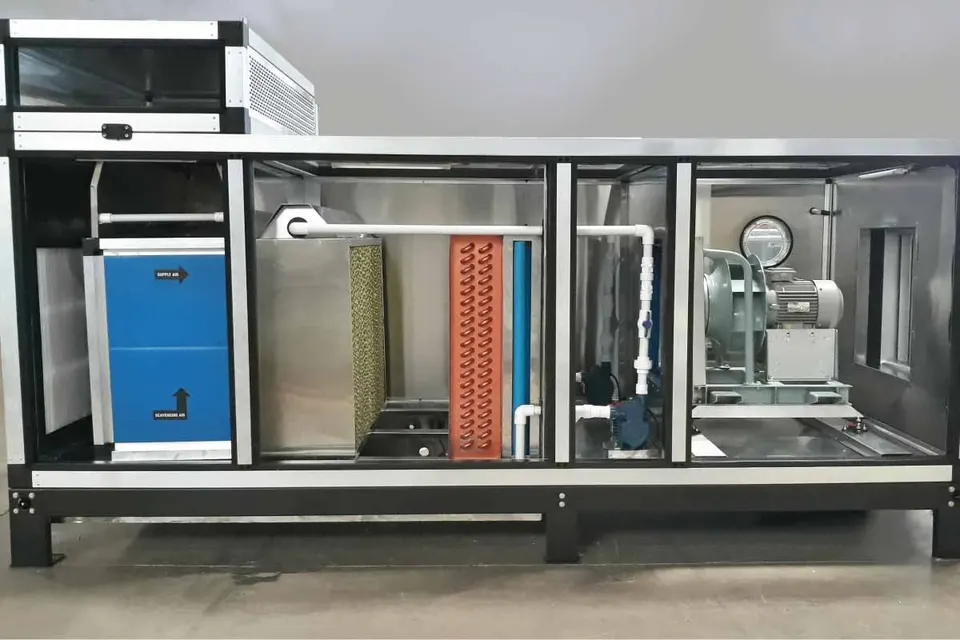
Two-stage Treated Fresh Air Units provide a complete solution for IEQ (Indoor Environmental Quality) and Energy Saving in a single modular unit based on the application with standard and add on features cooling, heating, humidification, high-efficiency filtration, mixing, sound attenuation, etc.
Two-stage TFAs also offer a unique heat recovery opportunity between incoming ambient air and building exhaust air without any cross contamination. Air to air heat exchanger can intake even toilet exhaust for heat recovery, which is not possible with traditional heat recovery wheels.
Fresh air cooling through Two-stage TFAs comes with many advantages. Two-stage TFAs are energy efficient and offer significant savings as compared to traditional HVAC units. They have the lowest connected loads with less than 30-40% energy usage, as only fans and low wattage pumps are required. They use 30 percent less water to deliver necessary cooling using conventional evaporating cooling. They also have a competitive lifecycle cost with lower operational cost, decreased power backup sizing and minimal maintenance costs. All of this results in long term savings in terms of operational expenses at a fractional increase in CAPEX and the inclusion of a new innovative step can deliver energy savings of up to 30-40 percent.
The first stage of these unique 2 stage TFA s is called Indirect evaporative cooling (IEC) which uses SensiCool air to air heat exchangers for sensible cooling of the ambient air, this innovative step pre cools air at as low as 200 W per Tr of cooling. This stage pre cools the air by removing 60 to 70% of the sensible load which is followed by a cooling coil (DX/CW). Sensible cooling in the first stage reduces on-coil air temperature, which in turn results in the reduction of the total required cooling load on the coil and measurable energy as well as cost saving through overall HVAC circuit from a reduction in the necessary capacity of other components.
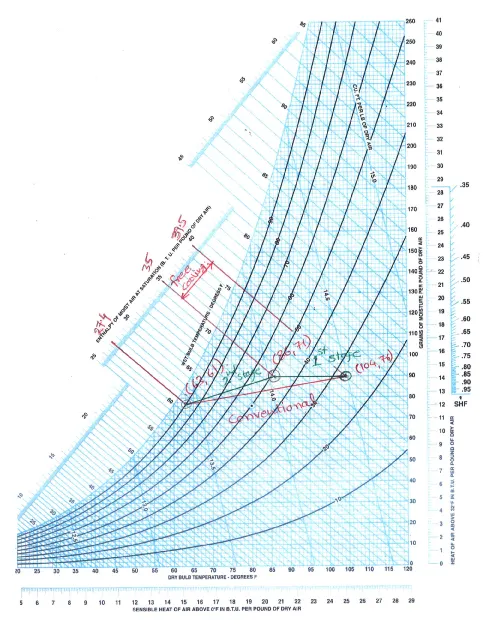
As shown in above psychrometric chart ambient air temperature is 40 DB and 24.4 WB and required off coil air temperature is 17 DB and 16 WB. For air flow of 30,000 cfm.
I'll use a case study of a hospital from Pune to illustrate.
Scenario 1: Using only Cooling Coil Coil load = M.Cp. ΔH = 30,000 x 4.5 x (39.5-27.4) / 12,000 = 136 TR
Scenario 2: Cooling coil with pre-cooling heat exchanger Coil load = M.Cp. ΔH = 30,000 x 4.5 x (35-27.4) / 12,000 = 85 TR
As illustrated, the cooling coil load was reduced by 37.5 percent as on coil air temperature changed from 40 degC to 29.8 deg.C in the case of the pre-cooling heat exchanger. This reduction, in turn, leads to reduced capital investment and operating cost by the reduced size of the evaporative coil as well as condensing unit capacity, piping diameters, control valves, etc.
The biggest advantage 2-stage TFAs have over other conventional heat recovery systems which makes this system suitable and applicable for all the TFAs that even in the absence of building exhaust (cooled air-which is mandatory to have for heat exchange in heat recovery wheel system), it can operate with outside air and still give substantial saving based on the environmental conditions.
For example: with Ambient conditions - 40 DB / 24.4 WB the possible supply temperature by SensiCool HX with Ambient air as scavenger will be - 32 DB / 21.57 W which still gives saving around 25%.
This tweak comes with many benefits, including the induction of fresh air without loading the central air conditioning system. It can be integrated with other AHUs and HVACs to optimise power consumption. The most crucial advantage, apart from cost savings, is that it is sustainable and eco-friendly. As there are no CFCs involved, it has zero ozone depletion potential as there is no contribution to greenhouse gases.
We would be happy to answer your queries on our TFA units.