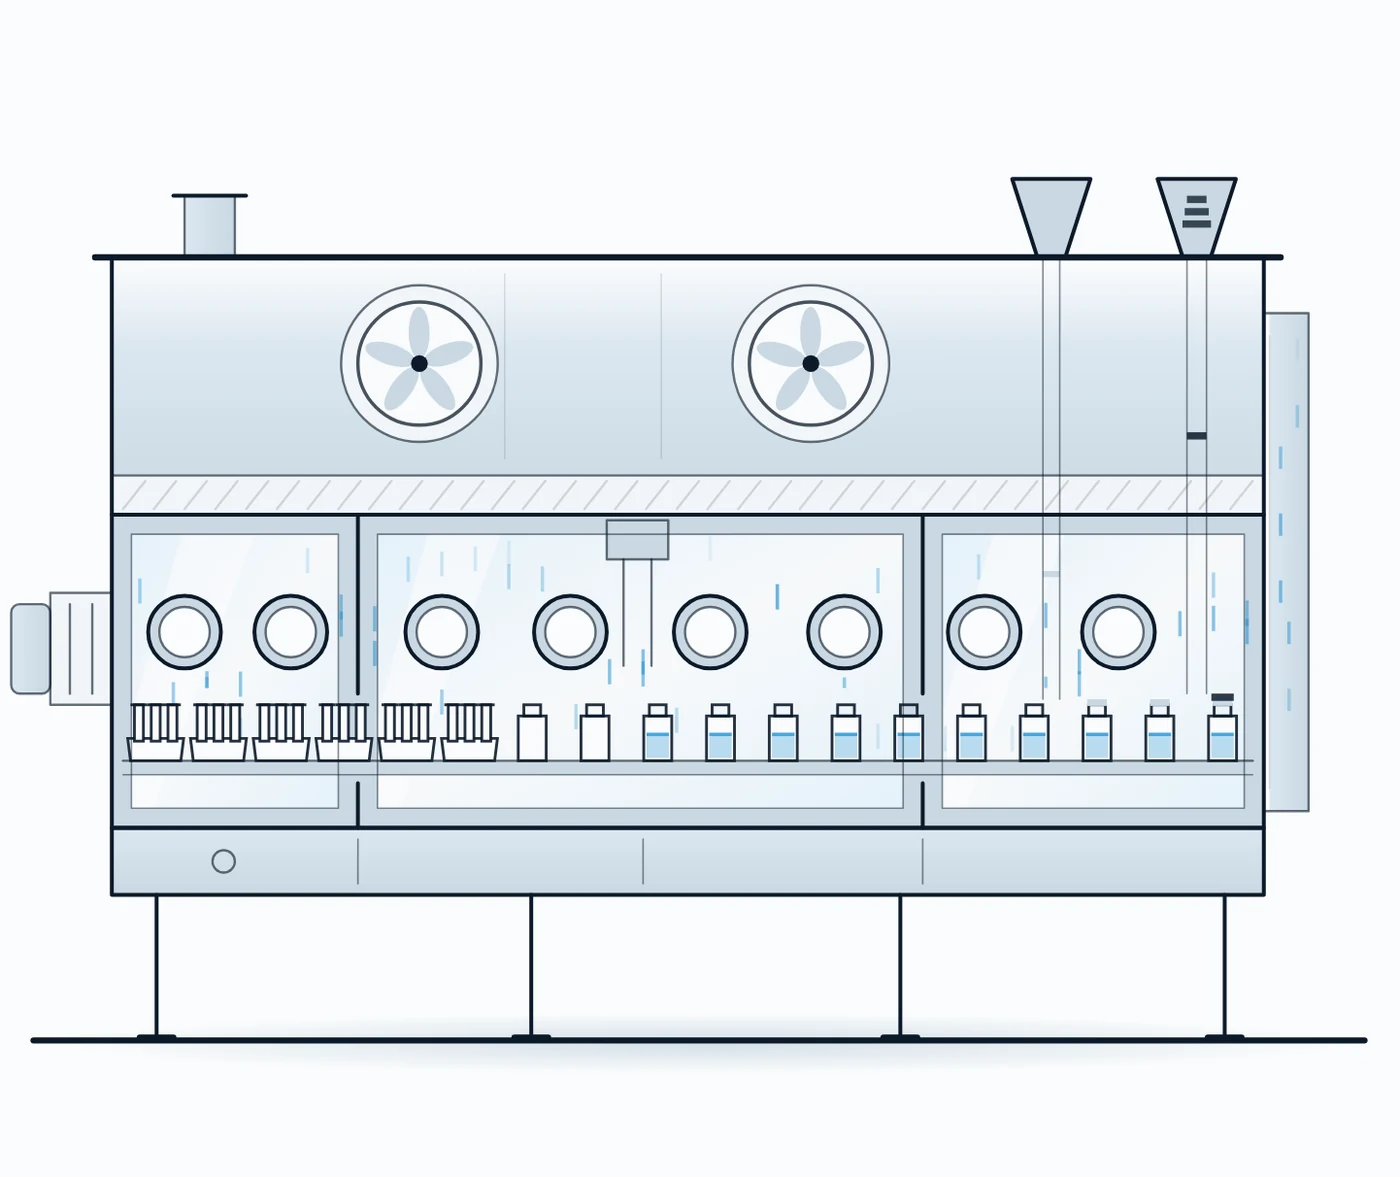
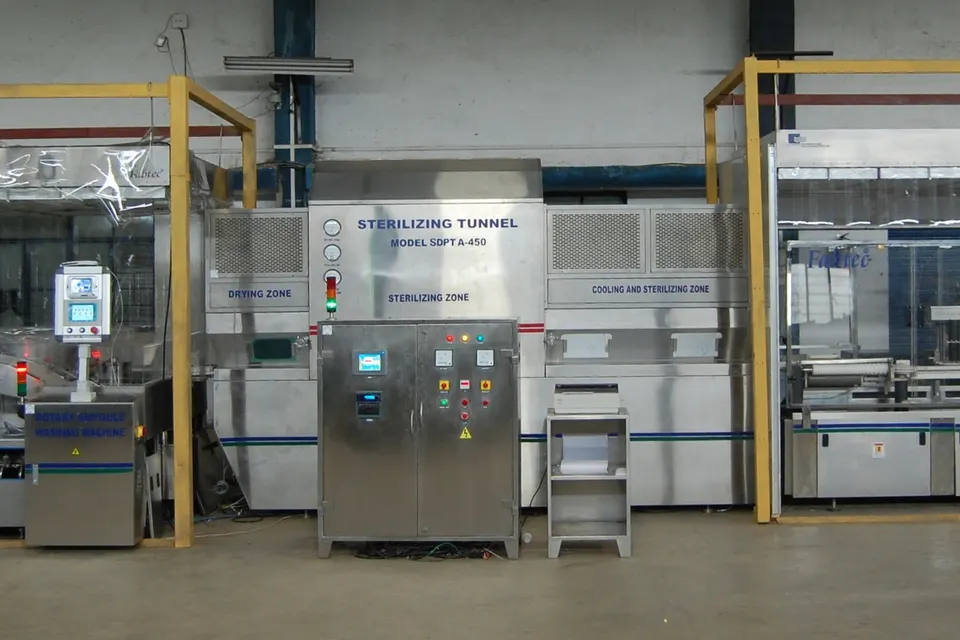
Mainly used in the sterilisation of vials for aseptic filling, this process is also useful when sterilising assembled and packaged materials, as heat conduction does not require the contact of the product with steam or water. The depyrogenation process varies depending on the load and product being sterilised.
Sterilising & Depyrogenation Tunnels are an integral part of the continuous automated high yield injectable line. They are used to ensure glass containers are sterilised and depyrogenated for filling operations as per 21 CFR part 211.92 guidelines.
While in the tunnel, glass containers are subjected to controlled heating and cooling cycle under ISO 5 cleanliness levels. The temperature of the glass container is raised and maintained for a prefixed value - the time required for the necessary reduction of the bio-burden within the tunnel enclosure. Downstream, the tunnel is integrated with a washer, and a filling machine upstream.
The Sterilising & Depyrogenation Tunnel comprises an endless variable speed conveyor; varying air modules including pre-heat, sterilising and cooling and stabilising; electricals, instrumentation and control system; as well as an interface between the washer-tunnel and tunnel-filling machine.
Fabtech's Sterilising & Depyrogenation Tunnels feature unidirectional air flow, process temperature progression curves, and reduced sterilisation times. The design allows for easy changes between different container types and configurations. The tunnels deliver repeatable accuracy required for successful validation, qualification, and reliable production capacity, and the controllable and reproducible process parameters simplify validation. There is easy access to tunnel interior for cleaning and maintenance.
We also offer the sterilisation of cooling and stabilising module by dry heat as optional feature.
The entire operation is controlled through PLCs which is 21CFR part 11 compliant with audit trail, featuring manual, automatic and night mode operations.
The Sterilising & Depyrogenation Tunnel has built-in monitoring and controls system for proper operation and appropriate interlocks with washer-filling machine to ensure smooth operation of integrated parenteral line for both vial and ampoules.
Every Sterilising & Depyrogenation Tunnel manufactured by us is subjected to rigorous testing as part of standard SAT protocol including 1. Velocity measurement and profile 2. HEPA integrity testing ( PAO test ) 3. Non- viable airborne particle count ( Cleanliness level ) 4. Temp profile ( Heat distribution and penetration ) 5. Endotoxin study 6. All interlock and controls
These tests are performed as per mutually agreed SOP and standard guidelines.
If you would like to know more about our Sterilising & Depyrogenation Tunnel or the SAT testing process, fill out the form below to request a call back from one of our experts.