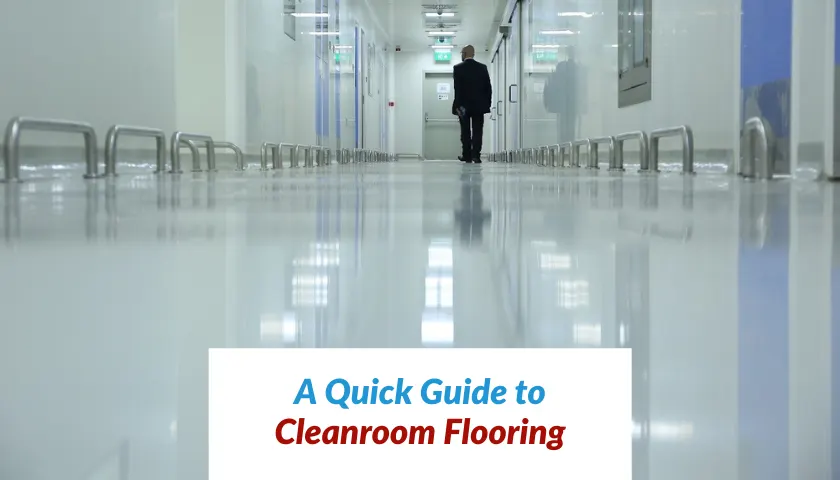
Therefore the emphasis on flooring is equally important for a cleanroom facility just like the Modular panel or the HVAC system, as flooring forms the internal area of the facility which is in direct contact with the environment of the cleanroom. Flooring should be chosen, keeping in mind the cleaning and contamination-free approach.
Here is a checklist of attributes for the floorings in cleanroom that is divided into:
- Physical attributes
- Chemical attributes
List of Physical attributes for cleanroom flooring:
- Cracks and gaps free
- Having coving between wall and floor,
- Seamless and impermeable finish
- Durable, and impact and abrasion-proof
- Chemical attack proof
- Temperature resistant
- Wear and tear-proof from cleaning agents
List of Chemical attributes for cleanroom flooring:
- Inert
- Low VOC generating
- Anti-bacterial
- Anti slippery
- Anti-static
- Variation in colour
Keeping in mind the above attributes, we can consider the following options to be used for Cleanroom flooring
- Epoxy flooring
- PU flooring
- Vinyl flooring
- Terrazzo flooring
- Vitrified tiles
After a thorough understanding of the flooring material, the selection can be carried out considering the probable activity in the cleanroom. The flooring material is selection is related to the activity in the cleanroom. In this article, I will be elaborating on the two most critical selections for Cleanroom flooring, i.e. Epoxy and PU flooring.
Let us look at an example to explain this. A pharmaceutical or semiconductor manufacturer will prefer Epoxy flooring for the production area, where even minute particles can adversely affect or cause product contamination. The other positives include anti-slippery, easy to clean and other attributes listed above. However, for testing laboratory or QC area, they may choose to with Vitrified Tiles as that this area may not necessarily be a cleanroom, and footfalls and movement may be higher than the production floor.
Post-production process involves the packaging of a finished product, thus contributing to excessive trolley and foot movement even higher than manufacturing. Such spaces require sturdy flooring like vinyl in this area. Likewise, a manufacturing zone with high movement terrazzo with cold welding be used for the more durable and longer solution.
The above examples illustrate the importance of suitable flooring material for cleanrooms. And two of the popular flooring solutions in the cleanroom for pharmaceutical, are Epoxy and PU.
Epoxy Flooring An Epoxy flooring offers protection to the floor surface simultaneously aesthetic enhancement too. The epoxy coating comprises of epoxy resins, and hardening compounds and their quick installation is ideal for restoring the concrete flooring showing signs of wear and tears with minor cracks and gaps, yet may not be seriously damaged. Epoxy coatings are easier to clean and maintain due to a chemical resistant surface, a density that offers durability, low porosity and seamlessness that is offers.
The Epoxy coating come in a variety of colours, allowing you to match your area differentiation. The application of the coating is between 1mm to 5 mm resulting in self-levelling flooring. The material movement is faster in the assembly areas and manufacturing areas(where the movement of trolleys and vehicles is moderate) due to the epoxy coating.
Epoxy coatings offer great resistance to chemicals yet for better stain protection urethanes may be an optimal choice. There are several variants of Epoxy coatings that may be chosen depending on the exposure to chemicals for corrosion control.
- Coatings for Concrete, Metal & Previously Coated Floors
- High-Gloss Reflective Coatings Available
- Wall Coatings
- Easy-to-Clean & Maintain
- 100% Solids & Waterborne Coatings Available
- Dense Seamless with Low Porosity
- All Colours Available
- Excellent Impact & Abrasion Resistance
- Environmentally Friendly
- Low Odour
thus making epoxy flooring a more popular option in flooring compared to other flooring solutions.
Poly Urethanes The speciality of Polyurethanes is they offer resistance to a wide range of chemicals including the ones to cause corrosion or abrasion like alkalis, alcohol, hydraulic fluids and many more. Advantages of using PU are
- Urethanes are equipped to endure heavy traffic (foot and trolley movement) and repeated cleanings and still provide a finished appearance.
- Polyurethane Systems can be applied to skid-inhibiting materials.
- UV Light Resistance
- High Gloss to Satin Finish
- Abrasion Resistance
- Stain Resistance
- Light Reflectance for Illumination of Workplace ( increase in LUX level)
- Excellent Gloss Retention
Raised Flooring Barring the above two, raised flooring is essential for non-pharma facility critical when it comes to cleanroom design. Raised access floors along with die-cast aluminium floating panels allow modification. This includes the thickness of the panels, varied size of hole configurations to achieve air volume and pressure differential and topcoat finish that offers chemical resistance. Hence they are specially employed in manufacturing pharma and semiconductors to maintain the laminar airflow from a HEPA filtered ceiling direct to the floor and a reliable base as a service access to the equipment.
Conclusion: Cleanroom Flooring Solutions require knowledge, planning, consulting, designing and engineering assistance. And Fabtech offers custom solutions based on the usage, and the contamination control and CGMP guidelines. To know more, please fill-up the form below.